
Air Pressure Level Switch for Cement & Fly Ash Loading
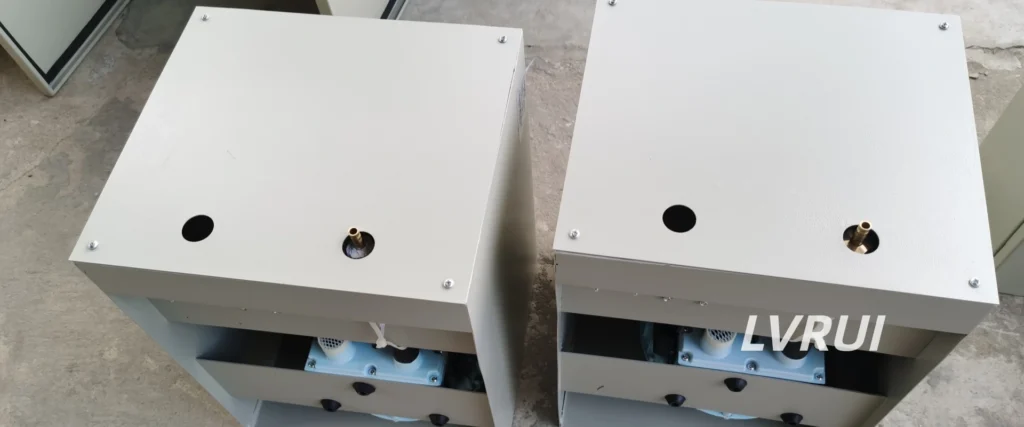
LRS-40 air-blow level switch for full-level detection and loading stop control
What Is an Air Pressure Level Switch?
An air pressure level switch is a full-level detection device used on cement loading spouts, fly ash loading systems and dry powder tanker loading systems. It is designed for dry powder and bulk solids such as cement, fly ash, mineral powder, lime powder and dry ash, not for liquid level detection.
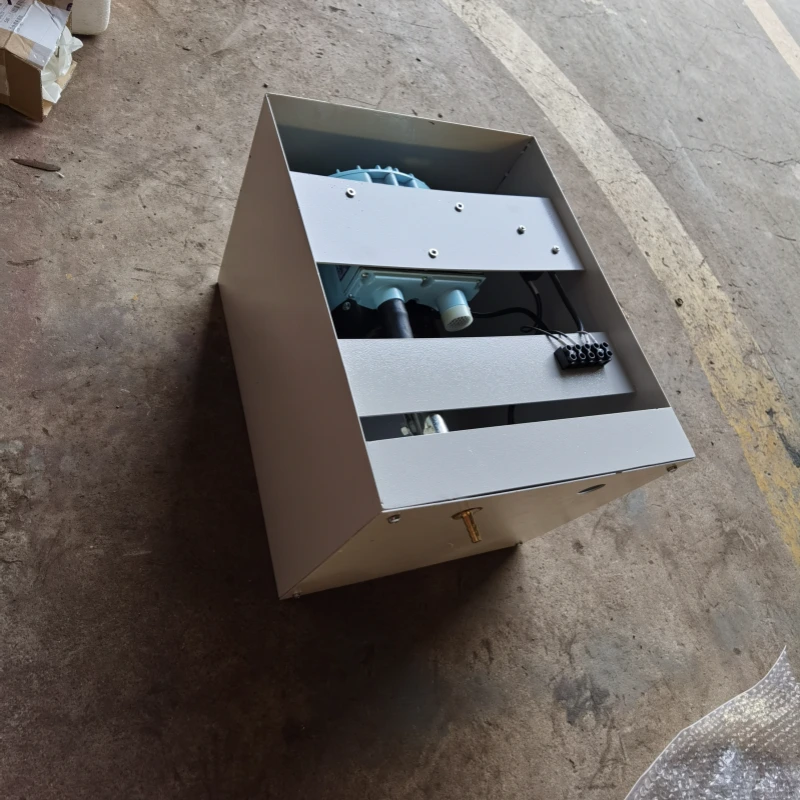
The device has a built-in air pump. During bulk loading, the pump sends air through a 10–12 mm tube to the lower blowing port of the loading head. When the loading head extends into the cement tanker and the powder blocks the blowing port, the air pressure changes. This pressure change is converted into an electrical switch signal and sent to the control cabinet.
After receiving the full-level signal, the control system can command the connected feeding or flow-control valve to close and stop material feeding. This helps prevent tanker overfilling, dust leakage and material spillage during cement or dry ash loading.
For a complete cement tanker loading system integrating material flow control, loading, dust collection and level detection, see our Cement Bulk Loader.
Working Principle
- The cement loading spout is lowered into the tanker inlet.
- The air pressure level switch starts working together with the bulk loader.
- The built-in air pump sends air through the tube to the blowing port at the lower center of the loading head.
- During normal loading, the air outlet remains open and air flows into the tanker.
- When cement, fly ash or dry powder reaches the full level and blocks the blowing port, the back pressure changes.
- The pressure switch generates an electrical full-level signal and sends it to the loading control cabinet.
- The control system sends a closing command to the connected material valve or flow-control valve according to the configured interlock logic.
The actual material stopping time depends on the valve type, actuator response, control logic and material remaining in the discharge path. For a detailed explanation of how air-pressure full-level detection works during cement tanker loading, see our guide to cement tanker level switches.
Main Specifications
| Item | Specification |
|---|---|
| Product name | Air Pressure Level Switch |
| Application | Cement loading spout, dry ash bulk loader, tanker loading system |
| Detection method | Air-blow pressure detection |
| Power supply | 220V |
| Output signal | Switch signal |
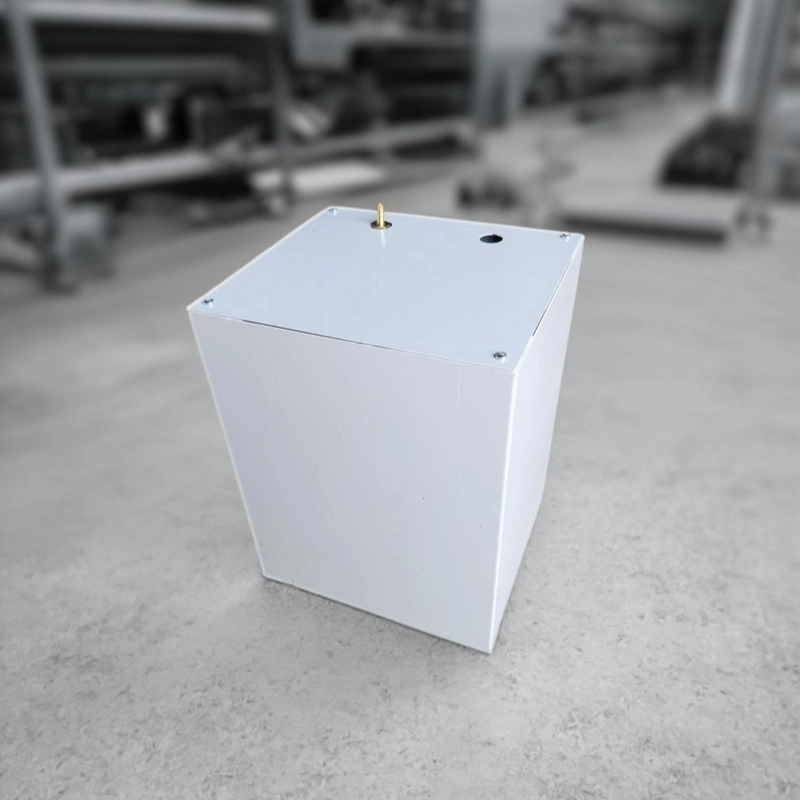
| Enclosure material | Powder-coated carbon steel |
| Installation position | On the lifting platform of the bulk loader |
| Air tube size | 10–12 mm |
| Air tube connection | Connected to the air inlet of the loading head |
| Blowing port position | Lower center of the loading head, extending into the tanker |
| Control response | Full-level signal sent to the control system; valve closure depends on the connected control and actuator |
| Suitable materials | Cement, fly ash, mineral powder, lime powder, dry ash |
| Main function | Full-level detection and overfill protection; provides a signal for loading valve shut-off |
Why Use an Air Pressure Level Switch?
✅ Designed for dry powder and bulk solids, not liquid level detection
✅ Built-in air pump for air-blow full-level detection
✅ No rotating paddle inside cement powder
✅ Full-level stop signal when the tanker reaches the detection point
✅ Helps prevent cement tanker overfilling
✅ Reduces dust leakage and material spillage during loading
✅ Suitable for cement, fly ash, mineral powder, lime powder and dry ash
✅ Easy to install on existing cement loading spouts and dry ash bulk loaders
✅ Can interlock with flow control gate, slide gate valve and control cabinet
Applications
The air pressure level switch is mainly used for full-level detection in dry powder tanker loading systems.
Typical applications include:
✅ Cement tanker loading
✅ Fly ash bulk loading
✅ Dry ash bulk loader systems
✅ Lime powder loading systems
✅ Mineral powder loading systems
✅ Cement silo discharge and truck loading stations
✅ Powder loading spouts with automatic stop control
✅ Bulk loading systems requiring overfill protection
Difference from Rotary Paddle Level Switch
| Item | Air Pressure Level Switch | Rotary Paddle Level Switch |
|---|---|---|
| Detection method | Air pressure change | Paddle rotation resistance |
| Contact with material | Only the blowing port contacts powder | Paddle works inside powder |
| Main application | Cement tanker full-level detection | Silo or hopper point level detection |
| Moving parts in powder | No rotating paddle in material flow | Rotating blade contacts material |
| Response during loading | Full-level switching signal for loading control | Depends on paddle contact condition |
| Best use case | Cement loading spout and dry ash bulk loader | Fixed silo or bin level detection |
Why It Is Suitable for Cement Tanker Loading
Cement tanker loading is a dusty and fast loading process. If the full-level signal is delayed or unreliable, cement powder may overflow from the tanker inlet, causing dust pollution, material loss and cleaning problems.
The LRS-40 is designed for this loading condition. The blowing port is positioned at the lower center of the loading head and extends into the tanker. When the powder reaches the preset detection point and blocks the air outlet, the resulting pressure change activates the pressure switch and generates a full-level signal.
This makes it especially suitable for cement loading spouts where automatic stop control is required.
For general application reference, point level detection can be used during truck loading to help prevent overfilling, including cement loading in dusty environments.
System Interlock
The air pressure level switch can be connected with the control cabinet of the bulk loader. When the full-level signal is triggered, the control cabinet can stop the loading process by controlling related equipment.
Common interlock equipment includes:
✅ Flow control gate
✅ Slide gate valve
✅ Loading control cabinet / PLC
This helps the whole loading system work in a safer and cleaner way.
Materials Handled
This product is suitable for dry powder and fine bulk solids, including:
✅ Cement
✅ Fly ash
✅ Dry ash
✅ Mineral powder
✅ Lime powder
✅ Dry powder materials with similar flow characteristics
It is not designed for water, slurry, oil or liquid level detection.
Installation Notes
The device box is usually installed on the lifting platform of the bulk loader. A 10–12 mm air tube connects the device to the air inlet of the loading head.
The blowing port should be arranged at the lower center of the loading head and extend into the tanker during loading. This position allows the switch to detect the full-level condition when the powder reaches the loading head outlet area.
Before installation, the air tube route, loading head structure and control cabinet signal connection should be confirmed according to the actual bulk loader layout.
Common Problems It Helps Solve
✅ Cement powder overflowing from the tanker inlet
✅ Operator cannot reliably judge the full level
✅ Loading valve receives the stop signal too late
✅ Existing bulk loading system needs automatic overfill protection
Air Pressure Level Switch FAQs
How does the air pressure level switch detect full level?
It uses a built-in air pump to send air to the blowing port on the loading head. When dry powder blocks the blowing port, the pressure changes. The device converts this pressure change into a switch signal and sends it to the control cabinet.
Where is the device installed?
The device box is installed on the lifting platform of the bulk loader. It is connected to the loading head through a 10–12 mm air tube.
What happens after the tanker is full?
When the full-level signal is triggered, the switch sends a signal to the control cabinet. The control system then sends a closing command to the connected valve according to the configured interlock logic. Actual valve closing time depends on the valve type, actuator response and material remaining in the discharge path.
Can it be used for fly ash loading?
Yes. It can be used for fly ash, cement, dry ash, mineral powder, lime powder and similar dry powder materials.
Can it replace a rotary paddle level switch?
It depends on the application. For cement tanker loading and dry ash bulk loader full-level detection, the air pressure level switch is often more suitable because it does not use a rotating paddle inside the powder flow.
Can it work with a flow control gate or slide gate valve?
Yes. The switch signal can be connected to the control cabinet, which can interlock with a flow control gate, slide gate valve or other feeding valve to stop unloading automatically.
Need Help Selecting an Air Pressure Level Switch?
Send LVRUI your material type, tanker inlet dimensions, installation position, operating pressure, air-supply conditions and required control signal. LVRUI will confirm a suitable air pressure level switch configuration for cement tanker loading and overfill protection.
✅ Designed for cement, fly ash and similar dry powders
✅ Installation position matched to the tanker loading arrangement
✅ Control signal configured for loader or PLC interlock