
Bulk Material Conveying Systems for Cement and Industrial Plants
Conveying equipment for powders, clinker, aggregates and other dry bulk materials
What Is a Bulk Material Conveying System?
A bulk material conveying system is a combination of equipment used to transport powders, granules or coarse bulk solids between storage, processing and loading points.
LVRUI supplies conveying equipment and coordinated equipment packages for cement plants and industrial bulk material handling applications. Depending on the material and project requirements, a system may include conveyors, feeding and discharge devices, flow control equipment, dust collection components and connections to downstream equipment.
Different materials require different conveying methods. Dry fine powders may be transported using air slide conveyors or screw conveyors, while clinker, aggregates and other coarse materials often require belt conveyors, chain conveyors or bucket elevators.
Key Features
✅ Multiple Conveying Methods
Air slide, screw, belt and chain conveyors, together with bucket elevators, are available for different material handling requirements.
✅ Material-Specific Equipment Selection
Equipment configurations are determined according to material properties, required capacity, conveying distance and operating conditions.
✅ Customized Equipment Connections
Conveyor dimensions, inlet and outlet arrangements, connection interfaces and installation layouts can be coordinated according to project requirements.
✅ Supporting Equipment Integration
Conveyors can be supplied with compatible feeding, discharge, flow control and dust collection equipment as required by the project.
Main Types of Conveying Equipment
Different conveyor types are used according to material characteristics, conveying direction, distance and required capacity. LVRUI supplies the following main equipment categories for cement production and compatible bulk material handling applications.
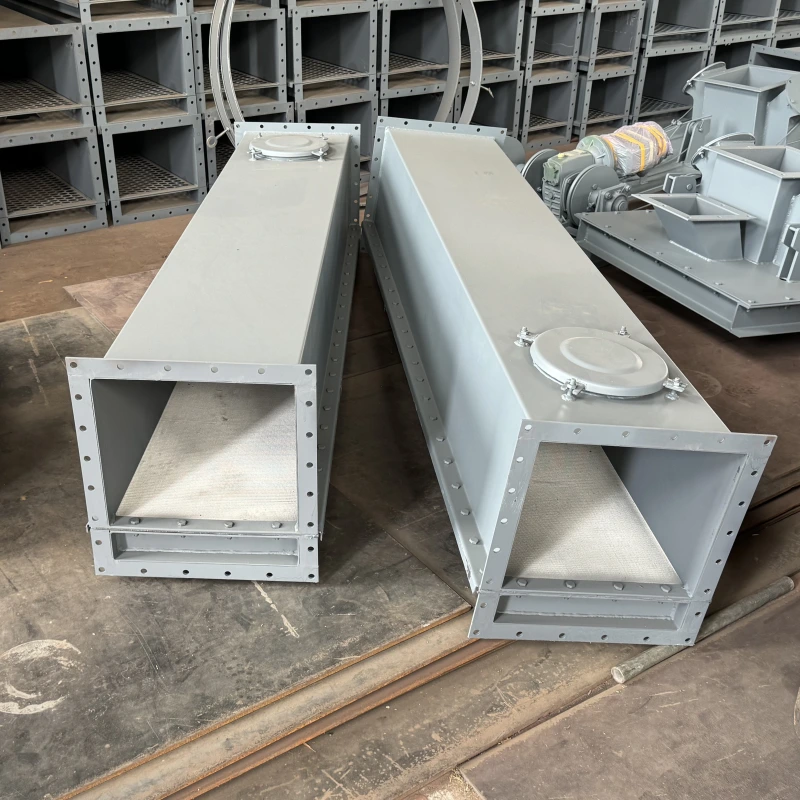
Air Slide Conveyor
An air slide conveyor transports dry, aeratable fine powders using low-pressure air and gravity.
Air passes through the air-permeable fabric to reduce resistance between powder particles, allowing the material to flow along a suitably inclined conveying trough.
Air slide conveyors are commonly used for cement, fly ash, raw meal and other compatible fine powders in cement plants, grinding stations and powder storage facilities.
They are particularly suitable for applications where a downward conveying route is available and the material can be adequately aerated.
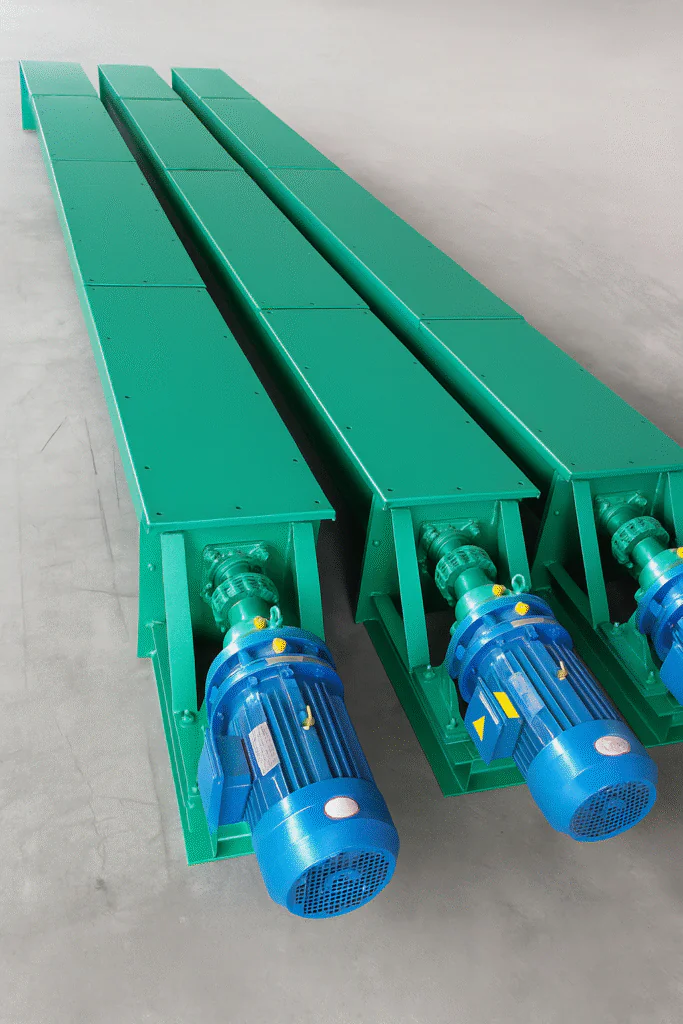
Screw Conveyor
A screw conveyor uses a rotating helical screw inside a trough or tube to move compatible dry bulk materials.
Screw conveyors are commonly used for short-distance powder transfer, controlled feeding and connections between silos, hoppers, dust collectors and processing equipment.
The conveyor diameter, screw pitch, conveying length and drive configuration depend on the required capacity and material properties.
Horizontal and inclined configurations can be supplied according to installation requirements.
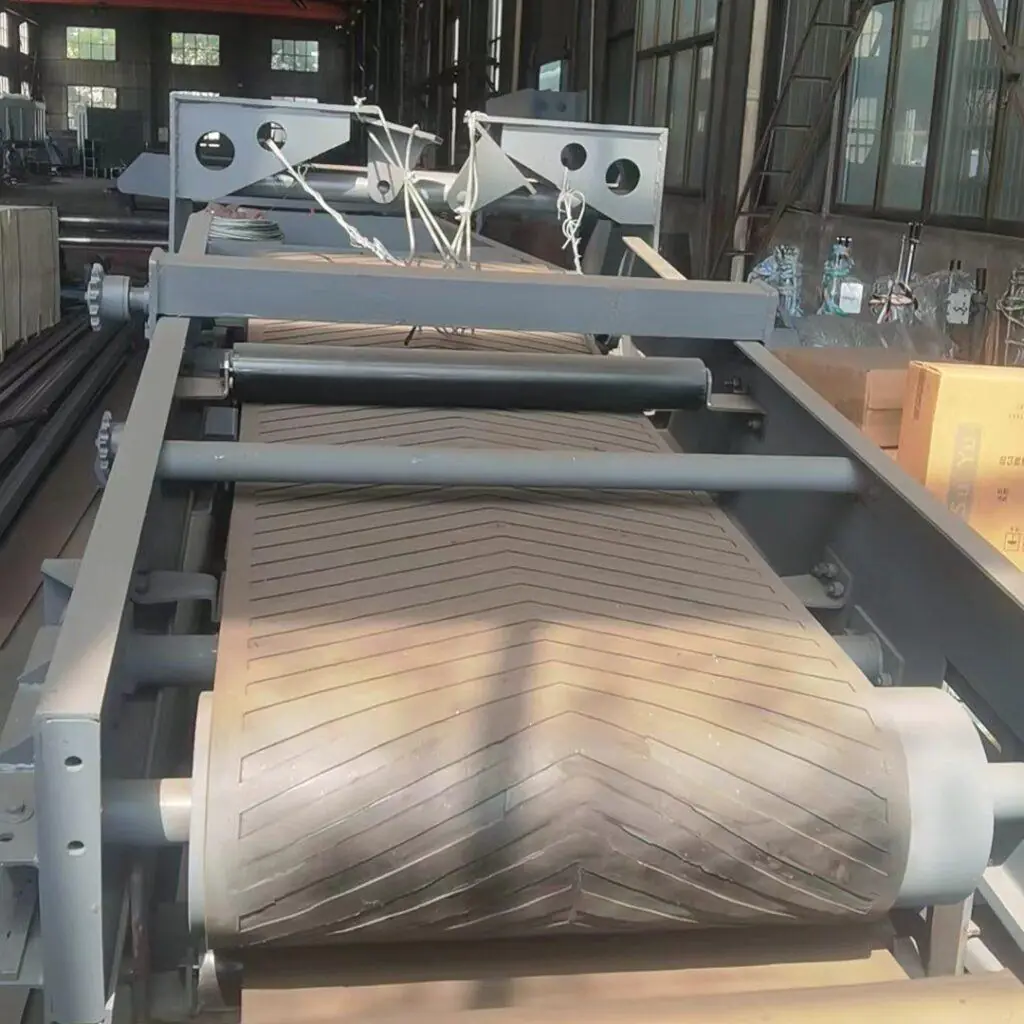
Belt Conveyor
A belt conveyor uses a continuously moving belt to transport bulk materials between loading and discharge points.
It is commonly used for clinker, limestone, aggregates, coal, sand and other compatible bulk solids, particularly where longer conveying distances or higher capacities are required.
Belt type, drive power, supporting structure and transfer-point arrangements should be selected according to material properties and operating conditions.
Dust collection or suitable enclosure arrangements may be required at loading and transfer points.
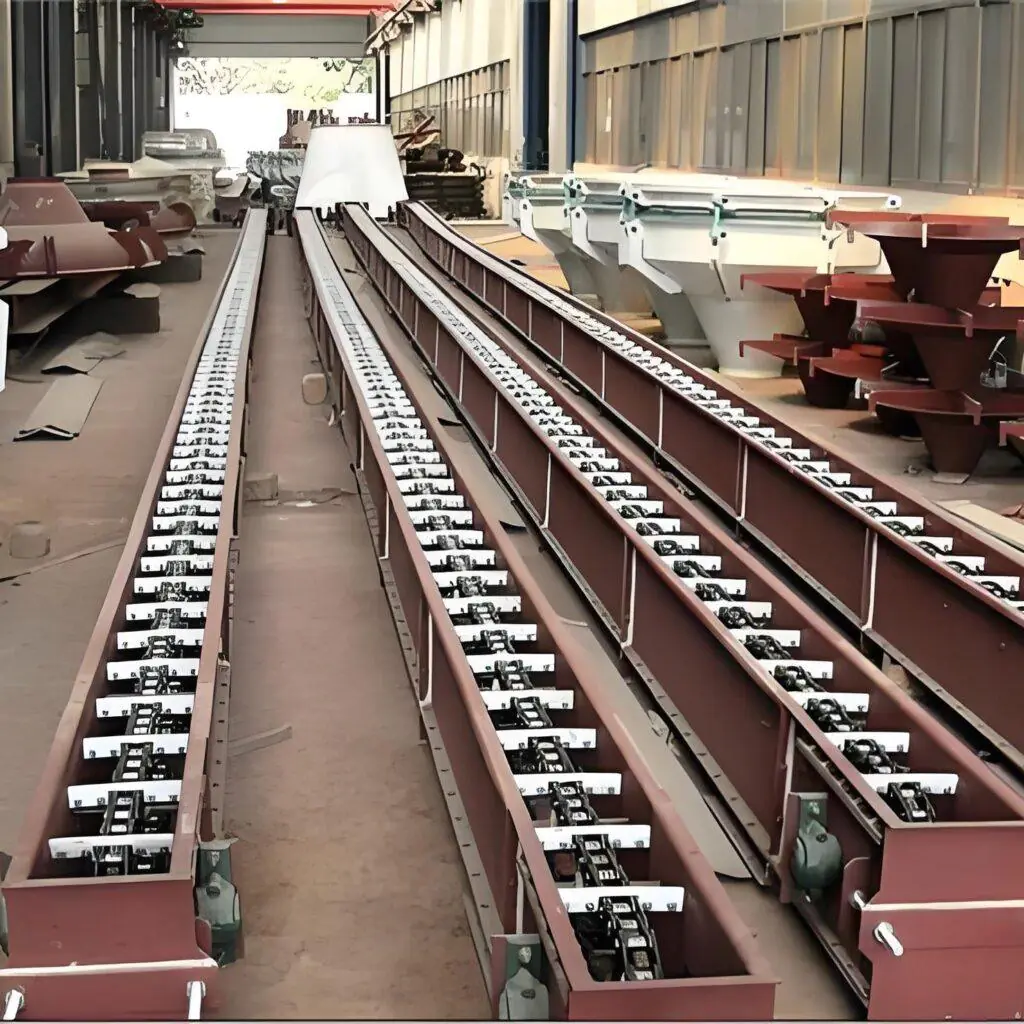
Chain Conveyor
A chain conveyor uses driven chains and scraper flights to move bulk materials through a conveying trough.
Enclosed chain conveyors can be configured for clinker, slag, limestone and other abrasive or coarse materials requiring horizontal or inclined transport.
The chain, scrapers, trough construction and wear-protection arrangements must be selected according to material temperature, abrasiveness, particle size and operating load.
An enclosed configuration can help contain dust and material spillage when properly designed for the application.
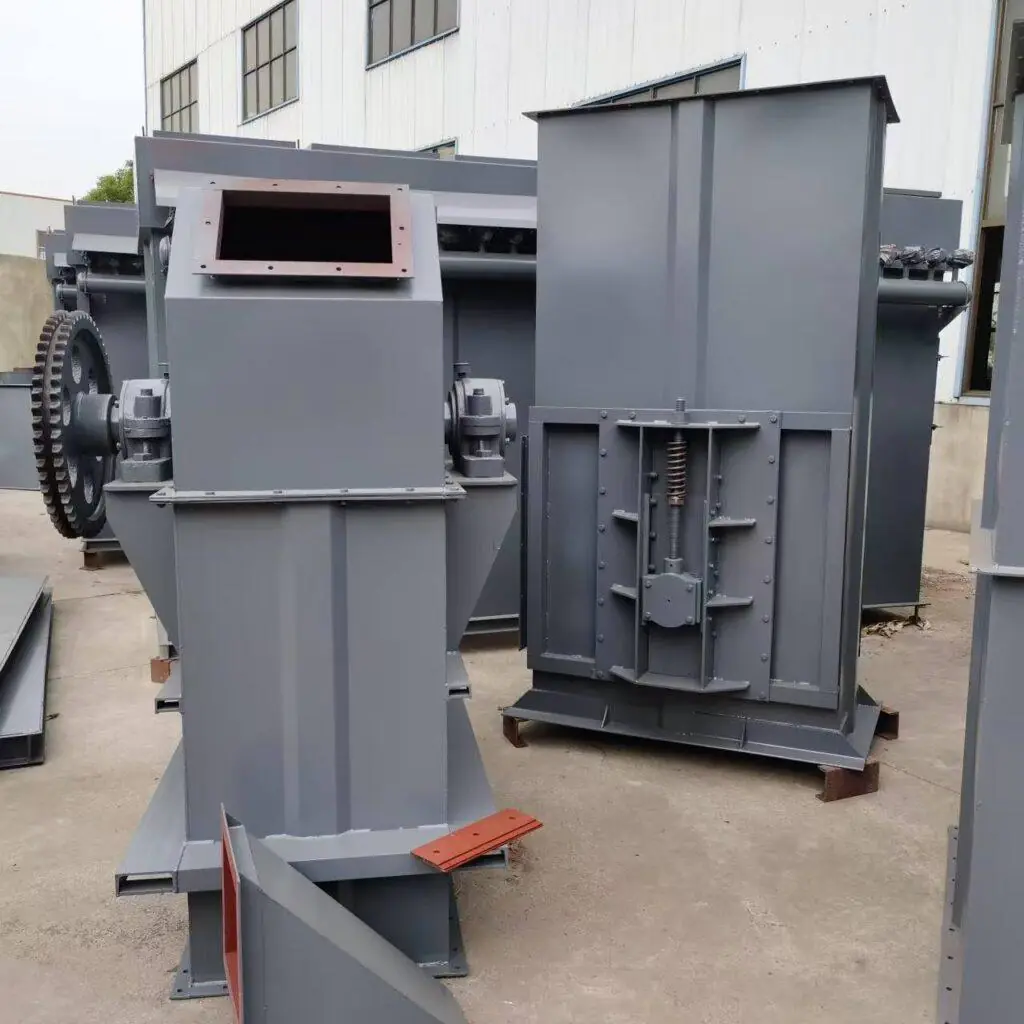
Bucket Elevator
A bucket elevator transports compatible bulk materials vertically using buckets attached to a belt or chain.
Bucket elevators are used to connect different process levels in cement plants, grinding stations, storage facilities and mineral processing lines.
They can be configured for cement, fly ash, clinker, limestone and other compatible materials according to the selected construction.
Equipment selection should consider lifting height, required capacity, material characteristics, temperature and the inlet and discharge arrangements.
How to Choose a Bulk Material Conveying System
Selecting a suitable bulk material conveying system requires an understanding of the material, required conveying route and operating conditions. No single conveying method is appropriate for every bulk material application. The following table provides a general comparison of common conveying requirements.
| Material or requirement | Typical equipment | Main consideration |
|---|---|---|
| Dry, aeratable fine powder | Air Slide Conveyor | Downward slope and aeration suitability |
| Short-distance powder transfer | Screw Conveyor | Length, capacity and material properties |
| Longer-distance coarse material transport | Belt Conveyor | Capacity, distance and transfer points |
| Enclosed conveying of abrasive bulk solids | Chain Conveyor | Wear resistance and operating load |
| Vertical material lifting | Bucket Elevator | Lifting height, material and capacity |
The final conveyor configuration must be confirmed according to the material properties, installation layout and operating requirements. Engineers should also consider upstream feeding conditions, transfer-point arrangements and the receiving capacity of downstream equipment.
Main Components of a Conveying System
A conveying system may include several interconnected equipment sections, depending on the process requirements. The main components and their functions are outlined below.
Feeding and Discharge Equipment
Material enters the conveying system from a silo, hopper, processing machine or other upstream equipment.
Feeding and discharge devices regulate or isolate the material entering the conveyor.
Depending on the application, these may include flow control gates, slide gates, rotary valves or other suitable equipment.
For dry powder feeding and regulation, see LVRUI’s Flow Control Gate Valve.
Conveying Equipment
The conveyor transports material between the designated inlet and discharge points.
Its configuration depends on the material, capacity, conveying distance, elevation difference and available installation space.
Multiple conveyors may be combined when the process requires horizontal, inclined and vertical material transfer.
Supporting Equipment and Powder Aeration
A bulk material conveying system may require additional equipment to maintain stable feeding, material discharge and conveying conditions. For dry fine powders such as cement, fly ash and raw meal, suitable aeration equipment can help improve powder flow at silo and hopper outlets.
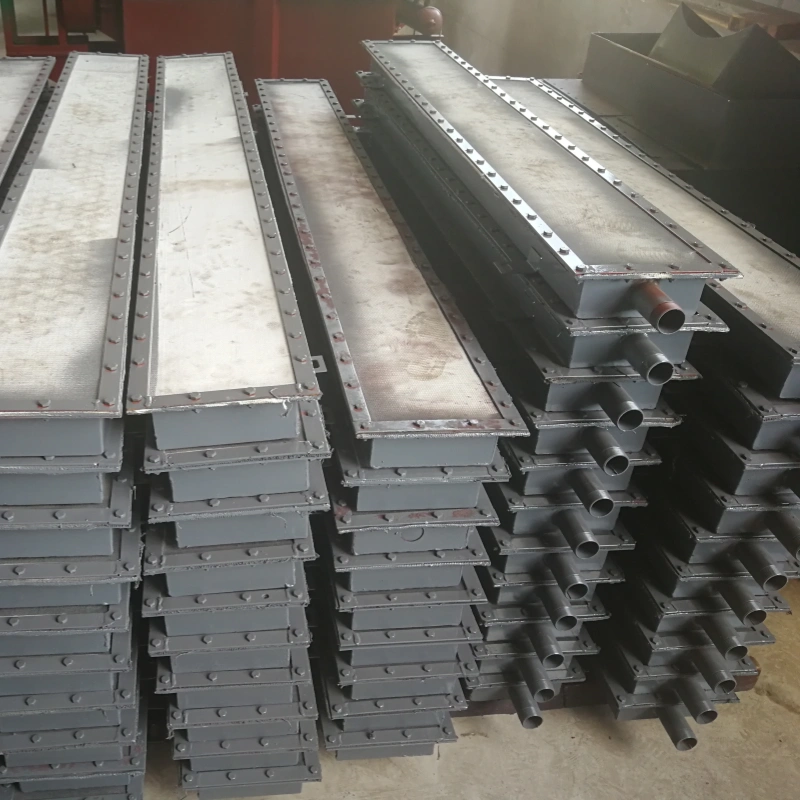
Aeration Pads
Aeration pads introduce low-pressure air into suitable areas of silos and hoppers. The air helps loosen compatible fine powders, reduce material compaction and improve discharge conditions.
They are commonly used as auxiliary equipment upstream of air slide conveyors, screw conveyors and other powder handling equipment.
Aeration pads do not transport material independently. Their primary function is to improve powder flow and support consistent feeding into downstream equipment.
Dust Collection and Material Containment
Dust control should be considered wherever fine powders are discharged, conveyed or transferred between equipment.
Depending on the conveying method, suitable measures may include enclosed conveyor sections, appropriately designed transfer connections and local dust extraction.
LVRUI also supplies dust collection systems for compatible cement and bulk material handling applications.
Downstream Equipment Connections
The conveying system must be compatible with the equipment receiving the material.
Depending on the process, downstream equipment may include storage silos, processing machines, packing equipment or bulk loading systems.
LVRUI can coordinate conveyor discharge connections with compatible bulk loading equipment when included in the project scope.
The final arrangement must be confirmed according to the approved process layout and equipment interfaces.
Conveying System Design Parameters
The operating performance of a bulk material conveying system depends on the selected equipment and actual working conditions. The following information is important when determining the equipment configuration.
| Parameter | Information required |
|---|---|
| Material properties | Material type, bulk density, particle size and moisture |
| Material temperature | Normal and maximum operating temperature |
| Conveying capacity | Required rate in t/h or m³/h |
| Conveying route | Horizontal length, inclination and lifting height |
| Installation conditions | Available space, inlet and outlet locations |
| Operating requirements | Continuous or intermittent operation |
| Dust control | Required material containment and extraction arrangements |
| Equipment interfaces | Upstream feeding and downstream receiving equipment |
Equipment dimensions, conveying speed, drive power and operating limits should be determined for each conveyor type. The complete system must also account for upstream feeding conditions, downstream receiving capacity and equipment interfaces. For coordinated equipment packages, connection dimensions and the proposed arrangement should be confirmed before manufacturing.
For additional industry background on conveyor engineering and safety resources, refer to the Conveyor Equipment Manufacturers Association (CEMA).
Typical Industries and Applications
LVRUI supplies conveying equipment for cement production and other compatible industrial bulk material handling applications.
Cement and Fine Powder Handling
Typical applications include transferring cement, fly ash and raw meal between grinding equipment, storage silos and downstream packing or bulk loading points. Equipment selection must account for material properties, dust containment and reliable feeding at each connection.
Clinker and Aggregate Handling
Typical applications include clinker transfer between storage and downstream processing or loading equipment, as well as limestone and aggregate handling between plant sections. Material abrasiveness, temperature and transfer-point design are important considerations.
Industrial Bulk Material Transfer
Other compatible mineral powders and dry granular solids may require horizontal, inclined or vertical conveying between processing and storage points. Equipment suitability should be verified according to the actual material properties and site conditions.
LVRUI Conveying Equipment Supply and Customization
LVRUI supplies standard and customized conveying equipment for cement plants and compatible bulk material handling facilities. Depending on the project, the equipment package may include multiple conveyors, feeding and discharge equipment, flow control devices, dust collection components and downstream connection equipment.
Available supply and customization capabilities include:
✅ Selection of conveying equipment according to material properties and operating requirements
✅ Customized conveyor dimensions, inlet and outlet arrangements and connection interfaces
✅ Coordinated equipment combinations and configuration drawings
✅ Factory assembly and inspection according to the approved equipment specifications
✅ Export packing and remote technical support
Final equipment specifications and supply boundaries are confirmed according to the customer’s process layout, operating requirements and approved drawings. LVRUI supplies the agreed equipment package and related configuration drawings. On-site installation is performed by the customer or their appointed contractor.
Bulk Material Conveying Systems FAQs
What is a bulk material conveying system?
A bulk material conveying system is a combination of equipment used to transport powders, granules or coarse bulk solids between storage, processing and loading points. It may include conveyors, feeding devices, discharge equipment, dust collection components and downstream connections.
What conveying equipment is suitable for cement powder?
Air slide conveyors and screw conveyors are commonly used for compatible dry cement powder. Air slides require suitable material aeration and a downward conveying slope, while screw conveyors are often used for short-distance transfer or feeding. Selection depends on the material and process layout.
Which conveying system is suitable for clinker and aggregates?
Belt conveyors, chain conveyors and bucket elevators may be suitable for clinker and aggregate handling. The choice depends on particle size, abrasiveness, temperature, conveying distance, capacity and whether horizontal or vertical transport is required.
Can LVRUI supply a complete conveying equipment package?
Yes. LVRUI can supply coordinated conveying equipment packages with compatible feeding, discharge and supporting components according to the agreed project scope. Equipment configuration and connection drawings can also be provided. Customers or their appointed contractors are responsible for on-site installation.
How can dust escape be reduced during bulk material conveying?
Dust escape can be reduced through suitable enclosed conveying equipment, controlled feeding, appropriately designed transfer connections and dust extraction at relevant emission points. The required measures depend on the material, conveyor type and operating conditions.
What information is required for a conveying system quotation?
Customers should provide the material name, bulk density, particle size, moisture content, temperature, required capacity, conveying distance, lifting height, installation layout and upstream and downstream equipment details. Existing process drawings and site photographs are useful when planning equipment combinations.
Request a Conveying System for Your Project
If you need conveying equipment for cement, clinker, aggregates or other bulk materials, please provide your material properties, required capacity, conveying distance and available installation drawings. LVRUI can review your requirements and recommend suitable conveying equipment and coordinated system configurations.
✅ Multiple conveying equipment types
✅ Customized equipment dimensions and connections
✅ Coordinated equipment packages and configuration drawings
✅ Export packing and remote technical support