
Powder Transfer System for Cement & Bulk Powder Handling
Integrated Conveying Solutions for Moving Dry Powder Materials Between Process Points
What is a Powder Transfer System?
A Powder Transfer System is a combination of conveying and material-handling equipment designed to move dry bulk powders from one process point to another. The system may include air slide conveyors, screw conveyors, bucket elevators, diverters, flow control devices and related feeding equipment according to the required transfer distance, capacity and process layout.
Unlike a single conveying machine, a powder transfer system focuses on the complete material movement route, including the feeding point, transfer equipment, discharge point and connection between different process stages.
Typical applications include transferring cement, fly ash, lime, raw meal and other compatible dry powders in storage, grinding, processing and loading systems.
How Does a Powder Transfer System Work?
A Powder Transfer System works by selecting suitable conveying equipment according to material characteristics, required capacity, transfer distance and plant layout.
The system receives powder from upstream equipment such as silos or hoppers, transfers it through suitable conveying equipment, and delivers it to downstream destinations including production equipment, storage equipment, process equipment or loading systems.
Depending on the application, the transfer route may include air slide conveyors, screw conveyors, bucket elevators, diverter equipment and supporting flow control devices.
The final configuration is determined by the material properties, conveying requirements and installation conditions.
Main Equipment Used in Powder Transfer Systems
Air Slide Conveyor
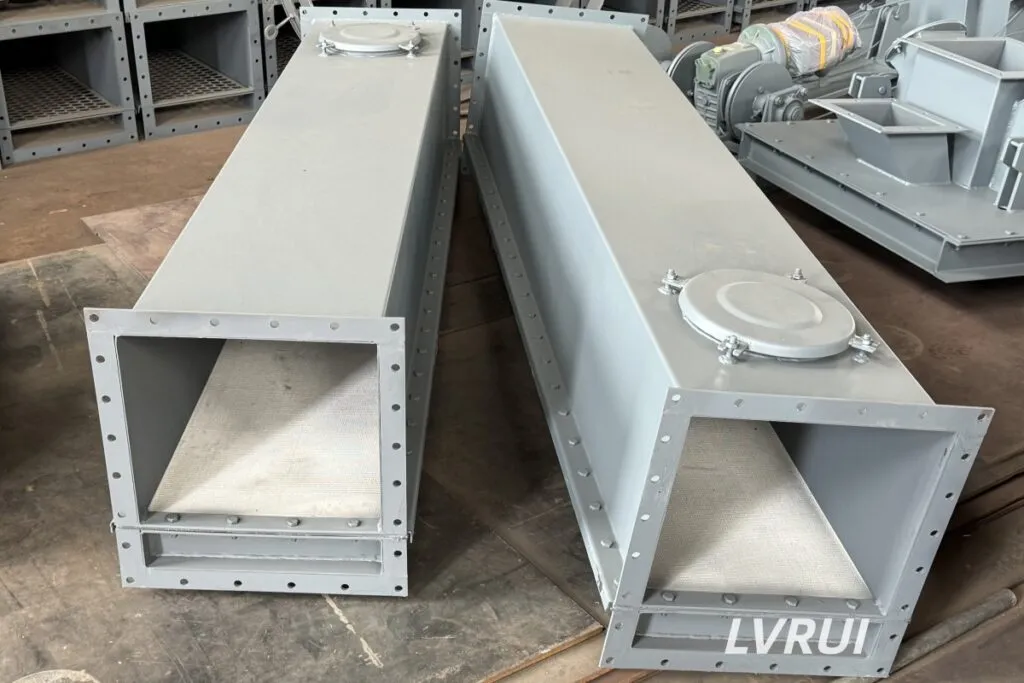
Air slide conveyors are commonly used for horizontal transfer of fluidizable powders over relatively long distances. They use low-pressure air passing through a permeable fabric or panel to maintain powder flow along the conveying route.
In a powder transfer system, an air slide conveyor is selected when the material characteristics, installation angle and required capacity are suitable.
Screw Conveyor Integration
Screw conveyors are often used in powder transfer systems where enclosed mechanical conveying is required, such as short-distance transfer, feeding points, vertical transitions or locations where layout limitations prevent the use of air slide conveyors.
Bucket Elevator for Vertical Transfer
When powder needs to be transferred vertically between different process levels, bucket elevators can be integrated into the system to handle continuous vertical movement.
Diverter Equipment
Diverter equipment allows one material source to supply multiple downstream destinations by directing powder into the selected transfer route.
Flow Control Equipment
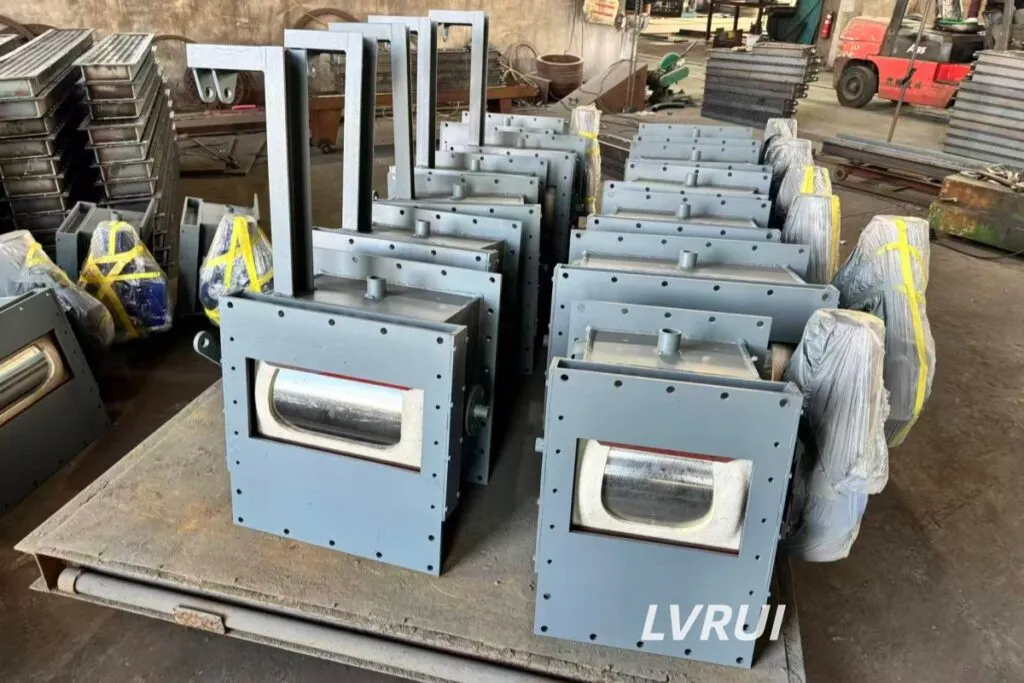
Flow control devices regulate the amount of material entering the transfer line and help match upstream discharge with downstream conveying capacity.
Optional Lump Breaking Equipment
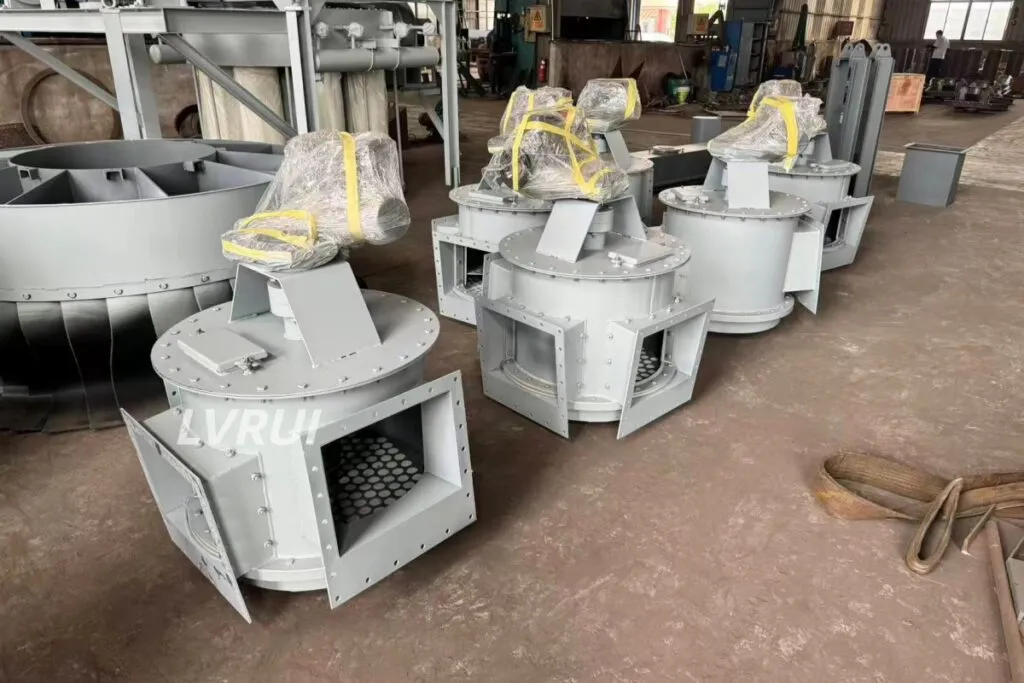
Lump breaking equipment may be considered when hardened lumps or compacted powder could affect valves, conveyors or downstream equipment.
Typical Powder Transfer Applications
Powder Transfer Systems are used in cement plants and other bulk material handling facilities to move dry powders between storage, processing, weighing and loading points. The final equipment combination depends on the material properties, transfer distance, required capacity and plant layout.
Cement, Raw Meal and Bulk Powder Transfer
Powder transfer systems are commonly used to move cement, raw meal, additives and other dry materials between storage silos, grinding systems, processing equipment and packing areas. These systems can also be integrated into complete Cement Bulk Material Handling Solutions.
Depending on the transfer distance and layout, the system may include air slide conveyors, screw conveyors, bucket elevators or other conveying equipment.
Powder Feeding to Process Equipment
In continuous production processes, powder transfer systems provide stable material feeding from storage units to weighing, batching or processing equipment.
The conveying arrangement is selected according to the required feeding rate, material flow characteristics and downstream process requirements.
Multi-Point Powder Distribution
When one storage source needs to supply multiple destinations, powder transfer systems can integrate diverter equipment and multiple conveying routes to distribute material according to production requirements.
Typical applications include supplying different production lines, storage areas or process units from a common powder source.
Powder Transfer for Loading and Packing Systems
Powder transfer systems can also be integrated with bulk loading equipment, packing machines and weighing systems to provide controlled material delivery before the final handling stage.
The system configuration should be matched with the capacity and operating requirements of the loading or packing equipment.
Typical Powder Transfer System Configurations
A Powder Transfer System is configured according to the material characteristics, required transfer route, capacity requirements and plant layout. Different combinations of conveying and routing equipment can be selected depending on whether the application requires continuous feeding, long-distance transfer, elevation change or multiple discharge destinations.
Configuration 1: Silo to Production Equipment
Typical Layout:
Silo → Flow Control Gate → Air Slide Conveyor → Production Equipment
This configuration is commonly used when powder stored in silos needs to be continuously transferred to downstream process equipment. A flow control device regulates the material discharge, while the conveying equipment moves the powder at the required capacity.
Typical applications include cement production lines, raw material feeding systems and continuous powder processing operations.
Configuration 2: Horizontal and Vertical Powder Transfer
Typical Layout:
Storage Bin → Screw Conveyor → Bucket Elevator → Upper Process Equipment
This arrangement is suitable for plants where powder needs to be transferred across different elevations or where installation space requires a combination of horizontal and vertical conveying.
The screw conveyor provides enclosed horizontal transfer, while the bucket elevator lifts the material to a higher process point. The final equipment combination depends on material properties, capacity requirements and layout conditions.
Configuration 3: Multi-Destination Powder Distribution
Typical Layout:
Silo or Storage Equipment → Diverter Equipment → Multiple Transfer Routes
When one powder source needs to supply different downstream destinations, diverter equipment can be integrated into the transfer system to select the required conveying route.
This configuration is commonly used in plants where powder needs to be distributed between multiple production units, storage areas or loading systems.
Configuration 4: Integrated Powder Transfer with Loading or Packing Systems
Typical Layout:
Storage System → Conveying Equipment → Packing or Bulk Loading Equipment
For applications involving packing or bulk loading, the powder transfer system needs to be matched with the capacity and operating requirements of the final receiving equipment.
The conveying arrangement may include air slide conveyors, screw conveyors, flow control devices and other supporting equipment to achieve stable material delivery.
Powder Transfer System vs Individual Conveyor Equipment
| Item | Conveyor Equipment | Powder Transfer System |
|---|---|---|
| Purpose | Move material | Complete transfer route |
| Scope | Single machine | Multiple connected equipment |
| Selection | Machine parameters | Process requirements |
| Design focus | Capacity and structure | Material flow and system layout |
Information Required for Powder Transfer System Selection
✓ Material name and bulk density
✓ Particle size and flowability
✓ Required capacity
✓ Transfer distance and elevation difference
✓ Feeding and discharge points
✓ Installation space
✓ Downstream equipment requirements
Based on these conditions, LVRUI can determine the suitable conveying combination, routing arrangement and connection design.
Equipment selection should also consider recognized bulk material handling practices and the actual operating conditions of the material. Industry organizations such as CEMA provide general guidance for conveyor and bulk material handling applications.
Powder Transfer System FAQs
What is a Powder Transfer System used for?
A Powder Transfer System moves dry bulk powders between different process points by combining suitable conveying and handling equipment. It is commonly used for cement, fly ash, raw meal, lime powder and other compatible materials.
What is the difference between a Powder Transfer System and a conveyor?
A conveyor is a single machine, while a Powder Transfer System is a complete transfer arrangement including feeding points, conveying equipment, routing devices and discharge connections.
What equipment can be included in a Powder Transfer System?
Depending on the application, a system may include air slide conveyors, screw conveyors, bucket elevators, diverters and flow control equipment. The final combination depends on material properties, capacity and layout requirements.
Can different conveying equipment be combined in one system?
Yes. Different conveyors can be combined when the process requires horizontal transfer, vertical lifting, route switching or controlled feeding between multiple process stages.
What information is required for Powder Transfer System selection?
Selection normally requires material properties, required capacity, transfer distance, elevation difference, feeding and discharge points, installation space and downstream equipment requirements.
Is dust control part of a Powder Transfer System?
Dust control is not the main function of a Powder Transfer System. Enclosed conveying, dust collection or separate dust control equipment can be integrated according to the application requirements.
Discuss Your Powder Transfer Requirements
Send LVRUI your material properties, required capacity, transfer distance, installation layout and feeding/discharge requirements. LVRUI can recommend a suitable conveying combination and system configuration.
✓ Air slide, screw and bucket elevator integration
✓ Customized transfer routes
✓ Diverter and flow control options
✓ Technical drawings and remote support