Practical Guidance on Cement Powder and Clinker Conveying, Equipment Coordination, and Operational Challenges
What Are Bulk Conveying Systems in the Cement Industry?
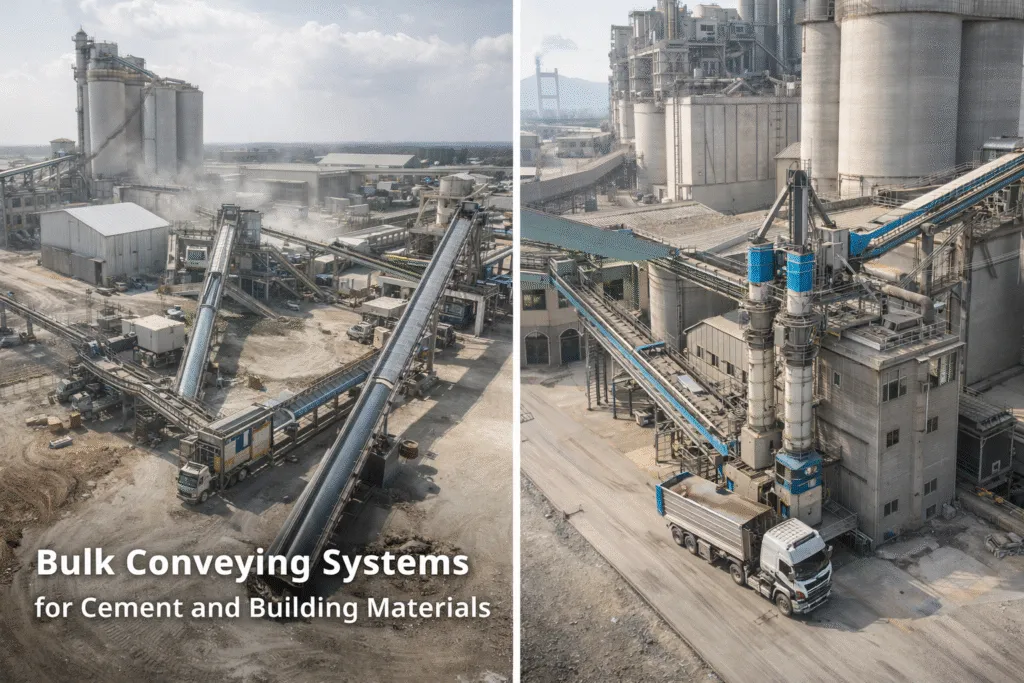
Bulk conveying systems in cement plants transport materials such as cement powder, fly ash, raw meal, clinker and limestone between storage facilities, processing equipment and loading points. Depending on the material and conveying route, these systems may use air slide conveyors, screw conveyors, belt conveyors, chain conveyors or bucket elevators.
A cement plant conveyor system must coordinate upstream discharge equipment with the actual throughput of each conveyor and the receiving capacity of downstream equipment. Material characteristics, required capacity, conveying distance, installation layout, dust-control requirements and operating conditions influence the overall system configuration.
Main Equipment Used in Cement Bulk Conveying Systems
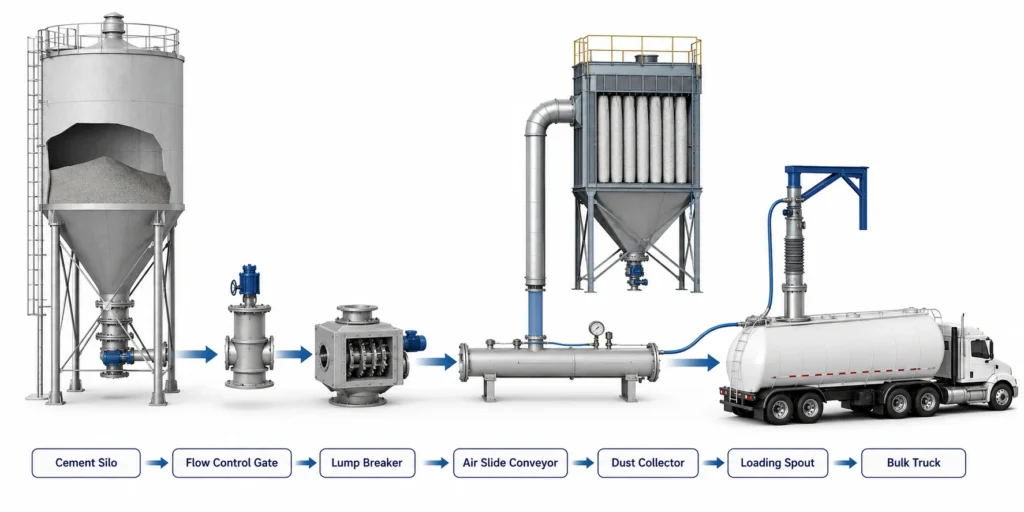
Bulk conveying systems combine several equipment functions. The actual configuration depends on material characteristics, the required conveying route and the connections between processing stages.
| System Function | Typical Equipment | Main Purpose |
|---|---|---|
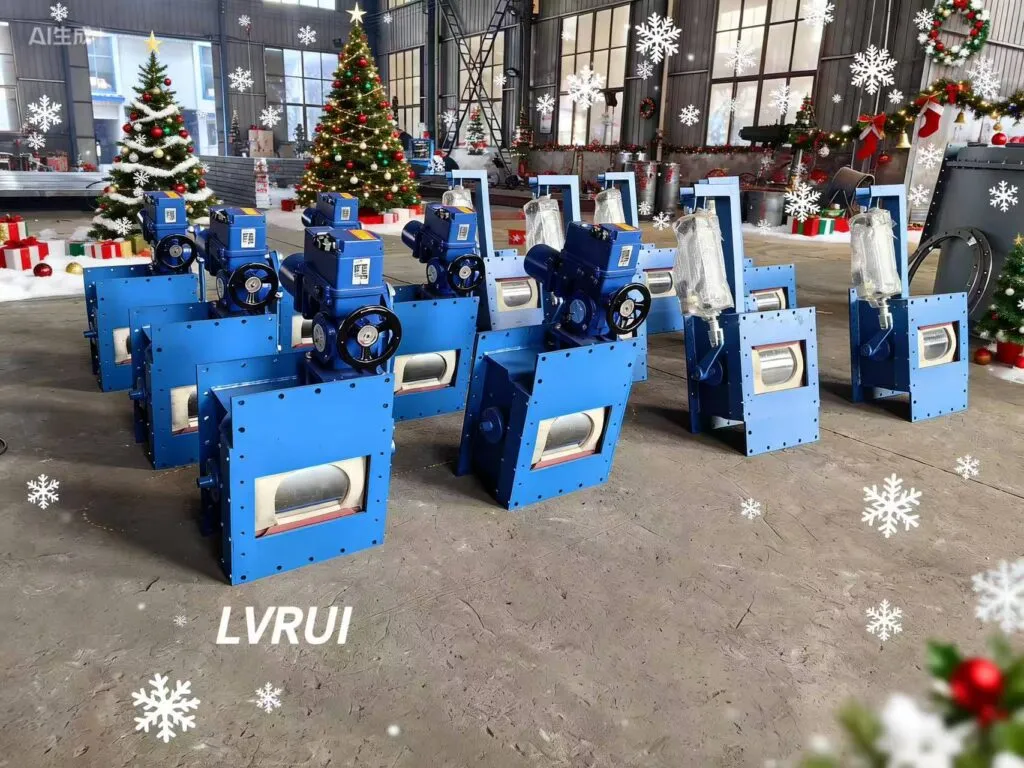
| Discharge and feeding | Flow control gate, shut-off gate, rotary feeder | Control or regulate material entering the conveying system |
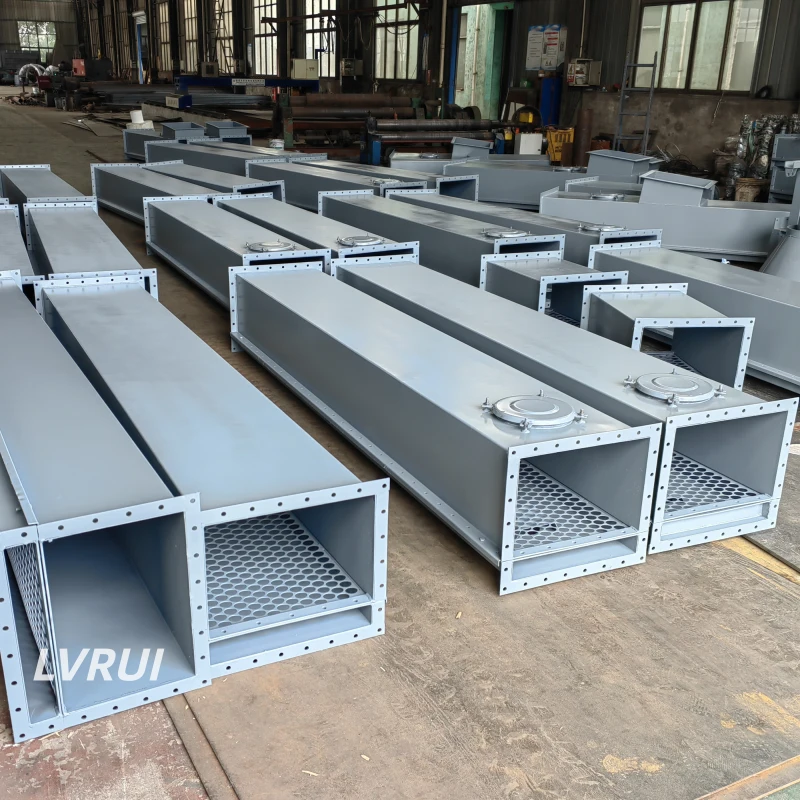
| Fine powder conveying | Air slide conveyor, screw conveyor, suitable pneumatic conveying equipment | Transfer compatible cement powder, fly ash and other fine materials |
| Clinker and coarse material conveying | Belt conveyor, chain conveyor, bucket elevator | Transport suitable coarse, heavy or abrasive materials |
| Dust extraction | Bag filter and compatible dust collection equipment | Collect dust at designated extraction points |
| Bulk loading interface | Loading spout and associated feeding equipment | Transfer material to the receiving vehicle or loading equipment |
| Auxiliary material preparation | Lump breaker, where required | Break suitable agglomerated material before it enters downstream equipment |
The listed equipment performs different functions and is not required in every installation. For example, a lump breaker should only be considered when material agglomeration presents a problem and the selected equipment is suitable for the material and process.
Air slide conveyors use low-pressure fluidizing air to help suitable fine powders move along an inclined conveying trough under gravity. They should be distinguished from positive-pressure or vacuum pneumatic conveying systems, which transport material through pipelines using a conveying gas stream.
For detailed equipment configurations and selection options, see LVRUI’s bulk material conveying systems page.
Typical Bulk Conveying Applications in Cement and Building Materials Plants
Bulk conveying systems are used at different stages of cement production and bulk material handling. Each application has different requirements for material characteristics, capacity, conveying layout and equipment connections.
Raw Material Conveying
Limestone and other raw materials are transported between receiving, storage, crushing and processing areas. Equipment selection should consider particle size, bulk density, conveying distance, required capacity and the actual operating environment.
Cement and Fly Ash Transfer
Fine powders such as cement and fly ash are transferred between grinding equipment, storage silos and downstream processing or loading points. Enclosed conveying arrangements, suitable feeding conditions and dust extraction at transfer points may be required.
Where the material is suitable for fluidization and the route provides sufficient downward inclination, air slide conveyors can be considered for powder transfer.
Clinker Conveying
Clinker conveying requires particular attention to particle size, temperature, abrasiveness and equipment wear. The conveyor and its transfer connections should be selected according to the material’s actual operating conditions.
Bulk Loading Operations
At the final conveying stage, material must be delivered to the loading equipment at a rate compatible with its receiving capacity. Discharge control, suitable transfer connections and dust extraction may be required to maintain stable loading operations.
Common Engineering Challenges in Bulk Conveying Systems
Bulk conveying performance depends on the interaction between the material, feeding equipment, conveyor and downstream receiving system. Problems in one part of the process can affect the performance of the entire conveying line.
Unstable Material Flow
Unstable feeding may cause fluctuating conveyor loads, material accumulation at inlets and interruptions in downstream operation. These problems can result from irregular silo discharge, changing material properties, unsuitable discharge control or a mismatch between feeding and conveying capacity.
When instability occurs, engineers should determine whether the problem originates at the storage outlet, within the feeding equipment or in the conveyor itself.
For detailed troubleshooting of silo discharge and feeding problems, see our material flow problems in cement plants guide.
Dust Generation During Conveying
Dust leakage may occur at conveyor inlets, transfer points, inspection openings and downstream discharge connections. Excessive material drop height, damaged seals, unsuitable enclosure arrangements or inadequate dust extraction may contribute to the problem.
Engineers should inspect the affected connection and assess the associated process conditions before modifying the extraction equipment. Suitable enclosures and correctly configured dust collection systems can help capture dust at designated emission points.
Equipment Wear and Maintenance
Conveying clinker and other abrasive materials can cause wear at transfer chutes, conveyor components and material impact areas. Wear rates depend on particle characteristics, temperature, conveying speed, transfer geometry and equipment materials.
High-wear transfer points may require replaceable wear liners, suitable impact protection and sufficient maintenance access. Regular inspections should focus on material impact areas, sealing components, drive equipment and locations where material accumulation occurs. Material temperature and particle characteristics should be verified before selecting protective components.
Engineering Practices for Reliable Bulk Conveying
Reliable bulk conveying requires coordination between material discharge, conveying equipment, transfer connections and downstream operations. Engineering decisions should be based on actual material properties and process requirements rather than the nominal capacity of individual machines alone.
Proper Discharge and Flow Control Design
Stable conveying begins with a feeding arrangement compatible with the conveyor’s actual operating capacity. When upstream discharge exceeds the conveyor’s receiving capacity, material may accumulate at the inlet or cause fluctuating loads.
Engineers should evaluate the required feeding rate, discharge opening, gate operating range and the conditions at the conveyor inlet.
Suitable flow control gates can regulate material discharge and help coordinate feeding with downstream equipment. However, they cannot independently solve bridging or other flow problems caused by unsuitable material or storage conditions.
Selection of Suitable Conveying Equipment
Conveying equipment should be selected according to material properties, required capacity, conveying distance, route geometry and operating conditions.
Air slide conveyors may be considered for suitable dry, fluidizable powders where the conveying route provides sufficient downward inclination. Screw conveyors can serve compatible short-distance transfer and feeding applications. Belt and chain conveyors can be used for suitable coarse-material transfer, while bucket elevators provide vertical material lifting.
For clinker and other abrasive materials, equipment selection should also consider temperature, wear resistance and the conditions at transfer points.
System-Level Integration
A conveying system must operate as a coordinated arrangement rather than a collection of separately selected machines.
Upstream discharge capacity, actual conveyor throughput and downstream receiving capacity should be evaluated together. Conveyor inlet dimensions, outlet connections, equipment operating sequences and maintenance access are also important.
When the conveying line connects to bulk loading equipment, the discharge rate must be compatible with the loading system. Suitable extraction connections and control signals may also be required.
Where multiple machines operate together, appropriate startup and shutdown sequences and equipment interlocks can help prevent overfeeding and material accumulation.
For loading equipment and its associated components, see LVRUI’s bulk loading systems.
Industry Standards and Engineering References
Bulk conveying equipment should be selected and configured according to the material characteristics, operating conditions, applicable technical standards and project-specific requirements.
For technical references on relevant conveyor equipment, engineers may consult the Conveyor Equipment Manufacturers Association (CEMA). The applicable standard should be determined according to the equipment type and project requirements.
FAQs About Bulk Conveying Systems in the Cement Industry
What are bulk conveying systems in cement plants?
Bulk conveying systems transport cement powder, fly ash, clinker, limestone and other bulk materials between processing, storage and loading points. Depending on the application, they may include mechanical or air-assisted conveyors, feeding equipment and connections to downstream facilities.
Which conveying equipment is suitable for cement powder?
Air slide conveyors can be used for suitable dry, fluidizable cement powder when the conveying route has sufficient downward inclination. Screw conveyors are another option for compatible short-distance transfer and feeding applications. The final selection depends on the material, required capacity, route and operating conditions.
What is the difference between an air slide conveyor and a pneumatic conveying system?
An air slide conveyor introduces low-pressure air through a permeable medium to help suitable fine powder move by gravity along an inclined trough. A pneumatic conveying system transports material through pipelines using a conveying gas stream.
The two technologies have different operating principles and should be evaluated according to the application.
Why is flow control important in bulk conveying?
Flow control helps coordinate material discharge with the receiving capacity of downstream equipment. Excessive or unstable feeding can cause conveyor overloading, material accumulation and interruptions in material transfer.
How can dust leakage be reduced during bulk conveying?
Dust leakage can be reduced through suitable conveyor enclosures, properly designed transfer connections, maintained seals and dust extraction at designated emission points. The appropriate measures depend on the dust source and actual operating conditions.
When should a lump breaker be used in a conveying system?
A lump breaker may be considered when stored or transferred material forms agglomerates that exceed the acceptable size for downstream equipment.
Its suitability and installation position depend on the material characteristics, lump size, process layout and maintenance requirements. It is not a mandatory component in every bulk conveying system.
Conclusion
Bulk conveying systems in cement plants must be configured according to the material characteristics, conveying route, required capacity and operating conditions. Different applications, from fine cement powder transfer to clinker conveying, present different requirements for feeding, dust extraction, wear resistance and equipment selection.
Reliable performance depends on coordinating upstream discharge, conveyor capacity and downstream receiving equipment. Evaluating these conditions as a complete process helps engineers identify suitable conveying arrangements and address recurring operational problems.
Need Help with a Cement Bulk Conveying Project?
If you are planning a cement powder, fly ash or clinker conveying project, share your material characteristics, required capacity, conveying distance and available installation drawings.
LVRUI can review your requirements and recommend suitable conveying equipment, discharge components and associated equipment configurations.
Please provide the following information when possible:
- Material type, bulk density and moisture condition
- Required conveying capacity and conveying distance
- Conveyor route, elevation difference and available layout drawings
- Upstream feeding and downstream receiving equipment
✓ Conveying equipment for cement and dry bulk materials ✓ Flow control and silo discharge equipment ✓ Compatible dust collection and bulk loading components ✓ Equipment configuration drawings and remote technical support
WhatsApp: +86 18261998937
WeChat: +86 18261998937
Email: info@lvrui-conveyor.com